

- info@prototypeshlh.com
- +86-133-9285-9203
- Room 2003, 20th Floor, Xingji Building, Shangde Road, Shajing Street, Bao'an District, Shenzhen
SERVICES

CNC Machining Service
Tight tolerances and finishing capabilities, as fast as 2 days.

Vacuum Casting Service
Production quality parts without the tooling investment.

Sheet Metal Fabrication
Experience the versatility 6 cost efficiency withflexible application options.

Die Casting Service
Create high quality custom mechanicals withprecision and accuracy.

Injection Molding Service
Production-grade steel tooling, as fast as weeks.

Carbon Fiber Manufacturing
Composite materials, such as carbon fiber reinforced plastics are highly versatile and efficient materials.
Popular Services

Injection Molding Service
A faster, easier way to order high-quality injection molded parts that accelerates iteration, testing, and scaled production. Upload your designs for DFM feedback and pricing in 24 hours.

3D Printing Service
Our 3D printing solutions cater to personalised needs with a diverse range of materials and colour options, including SLA, SLS, FDM, Projet, DMLS, and MJF printing services.

Surface Finishing
The easiest way to source your custom parts, with 15+ surface finishing options.

Design Guide
In-depth design guides full of best practices for all of HLH's manufacturing processes.

Case Studies
Success stories from innovativecompanies using HLH.

Blog
lndustry trends, company news andproduct updates.
Featured Posts
3D Printing vs. CNC Machining: Which is Better for Prototyping?
View more →
The Advantages of Projection 3D Printing for Mass Production
View more →
How to Choose Between Aluminum Alloy Casting and CNC Machining
View more →
What is Vacuum Injection Molding? What Type Suitable for Production?
View more →

About Us
Learn about our company, leadership, and mission totransform manufacturing.

Privacy Policy
Applies to all personal information collected through and/or processed in connection.

Contact Us
Our team is on stand by, waiting to assist you.

Videos
A large collection of educational videos and tutorials.

Aerospace & UAV
HLH is your 3D manufacturing partner from prototype to large scale production.

Consumer Products
New Product Introduction Solutions for Consumer Products.

Automotive
New Product Introduction Solutions for Automotive.

Industrial Machinery
The main purpose of industrial prototyping is to take the product from drawings into the real world.

Robotics & Automation
Need some assistance bringing your robotic device or parts from the sketch-board to reality?

Medical Devices
The medical industry needs high quality, dependable and safe parts and products.

Communications
We understand the demands and ever changing landscape of the communications industry.

Product Development
Industrial design and engineering consultancies are some of the most innovate and creative enterprises on the planet.

3D printing has made rapid prototyping faster and more accessible than ever. However, moving from an average-looking prototype to a flawless, production-grade 3D print requires a clear understanding of design optimization, material behavior, slicing parameters, and post-processing techniques.
Whether you are printing internal engineering brackets, clear optical lenses, or complex functional enclosures, this guide breaks down the essential steps to achieve pristine 3D printing quality every single time.
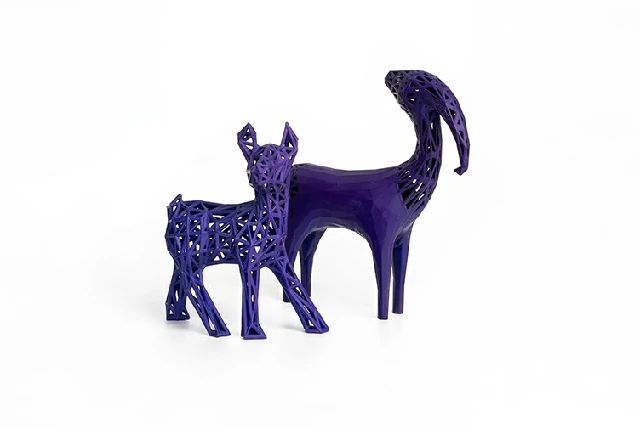
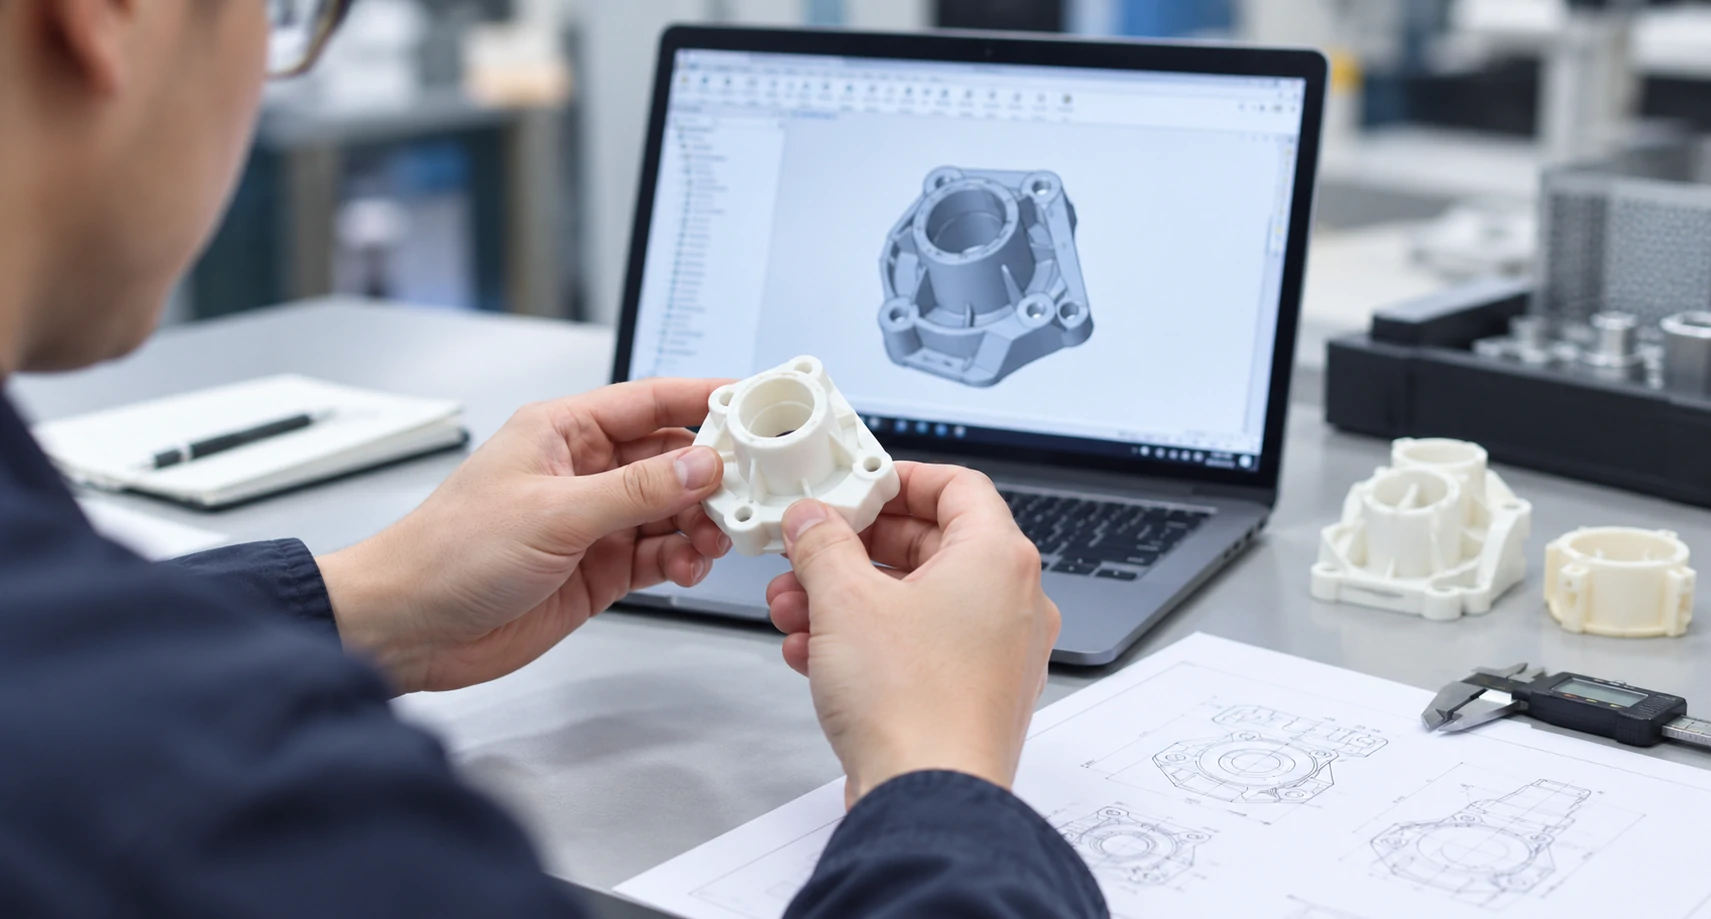
A perfect print starts long before the machine turns on. Designing specifically for 3D printing eliminates common defects like warping, layer separation, and support scar marks.
Maintain Uniform Wall Thickness: Avoid dramatic transitions between thick and thin sections to reduce thermal stress and sink marks.
Avoid Extreme Overhangs: Angles steeper than 45° require support structures. Where possible, redesign overhangs using self-supporting chamfers or fillets.
Design Proper Clearances for Moving Parts: For print-in-place assemblies, allow a minimum gap of $0.3\text{ mm}$ to $0.5\text{ mm}$ between mating components to prevent fusing.
Incorporate Escape Holes for Powder/Resin: For hollow designs in SLA or SLS printing, place drainage holes to allow uncured resin or un-sintered powder to flow out during cleaning.
Desktop 3D printers often struggle with consistency and tight tolerances. Choosing an industrial-grade additive technology tailored to your application is crucial for professional results:
3D printing technology | Best suited for | Key consideration |
|---|---|---|
Cost-effective prototypes, fixtures, and larger functional parts | Visible layer lines and direction-dependent strength | |
Detailed visual models and parts requiring fine surface detail | Resin properties and post-curing requirements | |
Complex polymer parts and functional prototypes | Powder-textured surfaces and process-specific tolerances | |
Functional polymer parts and small-batch production | Material selection, surface requirements, and part geometry | |
Metal prototypes and complex metal components | Build orientation, support strategy, residual stress, and finishing |
Proper orientation balances surface quality, strength, and print speed:
Prioritize Critical Cosmetic Surfaces: Position vital aesthetic faces facing upwards or away from support attachment points to eliminate tool marks.
Optimize Z-Axis Layer Height: Lower layer heights ($50\ \mu\text{m} - 100\ \mu\text{m}$) yield smooth curves, while thicker layers speed up build times for internal structural parts.
Manage Infill and Thermal Expansion: High infill density increases strength but raises internal stress during cooling. Use optimized honeycomb or gyroid patterns for structural stability.
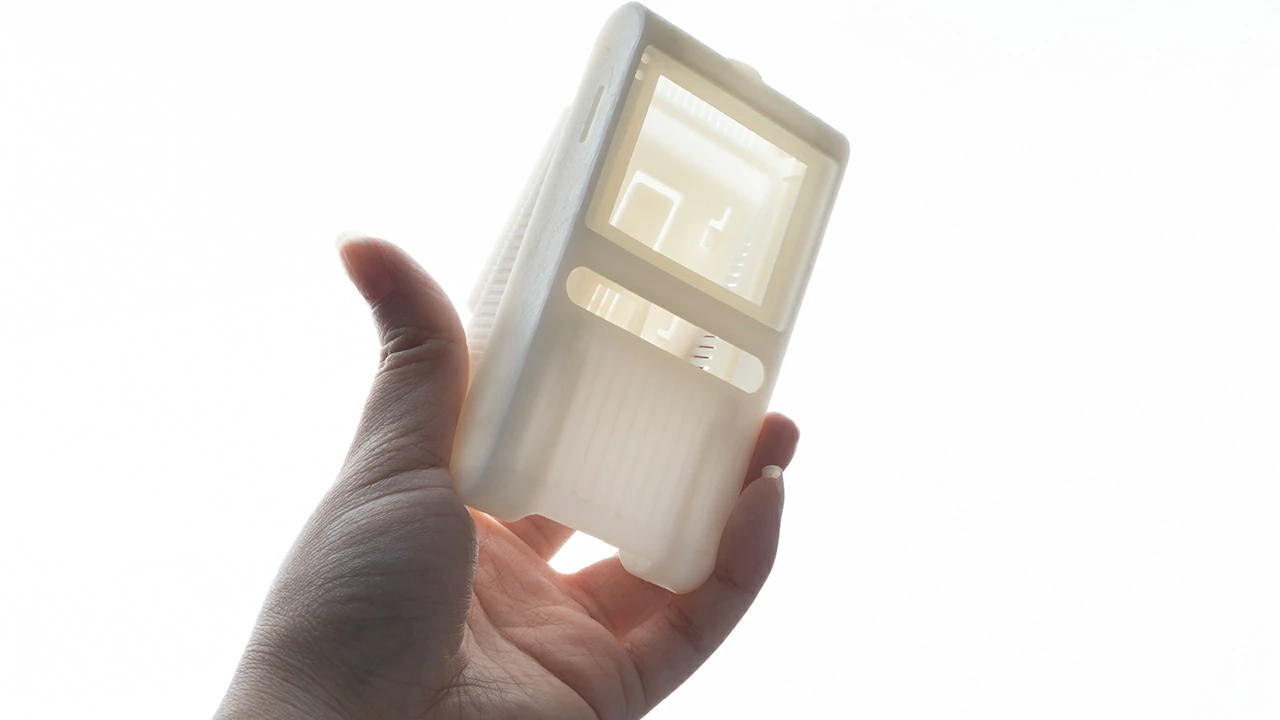
No 3D print is truly "perfect" straight out of the build chamber. Professional finishing brings parts up to end-use standards:
Support Removal & Sanding: Precision micro-sanding removes support stubs and smooths layer lines.
Vapor Smoothing & Media Blasting: Chemical vapor smoothing or bead blasting creates uniform surface textures across plastic parts.
Painting & UV Coating: Custom Pantone color matching, soft-touch coatings, or UV-resistant clear coats elevate aesthetics and durability.
Threaded Inserts & Machining: Heat-set brass inserts or secondary CNC reaming guarantee precise threads and bearing fits.
While 3D printing is ideal for rapid visual and functional prototypes (1 to 50 units), project requirements may call for hybrid manufacturing:
Mid-Volume Replicas (10 to 100+ Parts): Use a perfect SLA 3D print as a master pattern for Polyurethane Vacuum Casting to get production-grade polyurethane parts quickly.
Extreme Tolerances & Metal Precision: Combine metal 3D printing with 5-Axis CNC Machining for mating surfaces needing tolerances down to $\pm0.01\text{ mm}$.
Start with a valid CAD model, select an appropriate technology and material, optimize build orientation and supports, use suitable printing parameters, and inspect the finished part. The correct approach depends on the required accuracy, strength, surface finish, and intended use.
There is no single setting that determines quality. Model design, build orientation, material selection, layer height, supports, and machine parameters all contribute. For functional parts, orientation and load direction can be particularly important.
No. Smaller layer heights can improve the appearance of curved and angled surfaces, but they generally increase printing time. They do not automatically improve every dimension or guarantee stronger parts.
Choose a material suited to the application, design appropriate wall thickness and geometry, orient the part to account for its load direction, and optimize process-specific parameters. For FDM parts, layer adhesion and orientation are particularly important. Higher infill alone does not guarantee the best strength-to-weight ratio.
The answer depends on the material, geometry, build orientation, and finishing requirements. SLA is often suitable for fine surface detail and appearance models, while other technologies may be preferable for functional polymer parts or metal components. Post-processing can also affect the final surface.
Identify critical dimensions, follow the process-specific design guidelines, optimize orientation, and account for process variation. For mating features or tight tolerances, validate the design with a test part and use suitable measurement methods. Secondary machining may be appropriate for selected interfaces.
Yes. Depending on the material and process, 3D printing can produce functional prototypes for fit checks, assembly validation, and certain mechanical tests. However, printed-part properties may differ from those of the final injection-molded, machined, or otherwise manufactured component.
Consider injection molding when production volume, material requirements, repeatability, surface finish, and unit-cost targets justify the tooling investment. The appropriate changeover point depends on part geometry, mold cost, material, cycle time, and expected order volume.
Eliminate the trial-and-error of desktop printing and achieve industrial-grade quality on your first run.
At HLH Prototypes, we operate state-of-the-art SLA, SLS, and Metal SLM 3D printers alongside full-service post-processing and quality inspection setup. Coupled with our CNC Machining, Vacuum Casting, Sheet Metal Fabrication, and Rapid Injection Molding capabilities, we support your product lifecycle from concept validation to mass manufacturing.
Industrial Speed: Get high-precision 3D printed parts delivered in as fast as 24 to 48 hours.
ISO Certified Quality: Strict dimensional checks and CMM inspection reports available for every project.
Expert Engineering Support: Free Design for Manufacturability (DFM) analysis on every uploaded CAD file.
Ready to print your perfect prototype? Upload your CAD models to HLH Prototypes today for an instant quote and expert design evaluation.
SERVICES